

This memo addresses issues with chemical residue limit calculations when carried out on an equipment train basis. The key element to discuss is whether it is appropriate to separately calculate limits for each item in an equipment train based on the total batch size but using only the area for that specific equipment item in the train. Before that is discussed, we will cover the basis (conventional and common) approach of using both the total batch size and cumulative equipment area to derive one L3 limit (for example, in mcg/sq cm) that applies to each item in the train. For clarity, we will call this Case 1. After that, we will focus on potential issues if individual equipment areas are used for separate L3 limits. We will call these calculations Case 2. After discussing those Case 2 problems, we will balance those concerns by briefly mentioning Case 3 (a “stratified sampling” approach) which has elements of Case 2 but is a clearly different approach to setting limits. Stratified sampling has been previously covered in detail in memos of March, April, and May of 2010.
Each of these cases involves multiple equipment items used sequentially in the manufacturing process. Sequentially here means a situation where the product is processed first with Equipment A, and then Equipment B, and then Equipment C, and so on. [Note that if multiple equipment items are used for the same processing step, please consult the Memos of November and December 2016, dealing with a “split batch”, for how that might be handled.]
Generally for such a sequential equipment train, the Batch Size is for the total drug product processed in the manufacturing equipment. And the Surface Area is the total equipment surface for the entire train. That is, the sum of the areas of Equipment A, plus Equipment B, plus Equipment C, and so on. The typical limit calculation for cleaning validation for drug products is something like this:
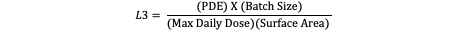
Where:
L3 is the limit of the API per surface area, typically in mcg per square centimeter (or per square inch)
PDE is the Permitted Daily Exposure of the active (API) in the cleaned drug product, which also could be expressed as ADE (Acceptable Daily Exposure) or perhaps 0.001 of the minimum therapeutic dose of the active (API) in the cleaned drug product
Batch Size is the maximum size (typically in mass or volume units) of the next drug product
Max Daily Dose is the maximum daily dose of the next drug product
Surface Area is the equipment product contact surface area (sq cm or sq in)
The above approach results in the same L3 limit for each of the equipment items in the train, which could be expressed in terms of L4a (mcg per swab), or L4b (mcg per mL of extracted swab solution), or L4c (mcg/mL or mcg/mL for rinse samples).
We have seen cases where, realizing that the difficulty of cleaning varies with each equipment item, firms will set surface area limits in a different way. This different way involves treating each equipment item separately utilizing the entire batch size but only the surface area of that specific equipment item for the L3 calculation. Unless each equipment item has the same Surface Area, the calculated L3 values will be different, which may (or may not) reflect any difference in terms of the difficulty of cleaning. Why is this problematic? The reason is that this Case 2 approach may result in a total carryover to the next product which may be unacceptable. Here is an example with just three equipment items, A, B, and C.
Let’s assume a PDE value of 2 mcg, a total batch size 200 kg (or 200000 g), a maximum daily dose of the next drug product of 1 gram, and with surface areas of 100000 sq cm for Equipment A, 150000 sq cm for Equipment B and 75000 cm for Equipment C. Examples below are calculations for the two approaches (cumulative versus individual surface areas) for both L3 and L2, with L2 being the total amount carried over calculated as “PDE X Batch Size”.
For a typical cumulative surface area calculation, here are the calculations for L3 and for L2. There is no need to calculate L4 values for either example because the relative difference illustrating potential problems is adequately expressed by L3 and L2 values.
Example 1 for Case 1: Cumulative Area Calculations
| Equipment | Surface Area (sq cm) | L3 (mcg/sq cm) | L2 (mcg) |
| A + B + C | 325000 | 1.23 | 400000 |
Note that the L2 could be reported as 400 grams (rather than micrograms).
If limits were calculated based on each individual equipment surface area, here are calculations for L3 and for L2
Example 2 for Case 2: Individual Area Calculations
| Equipment | Surface Area (sq cm) | L3 (mcg/sq cm) | L2 (mcg) |
| A | 100000 | 4.00 | 400000 |
| B | 150000 | 2.67 | 400000 |
| C | 75000 | 5.33 | 400000 |
| A + B + C | 1200000 |
Note what happens with this type of calculation is that the individual calculated L2 (the sum of each individual L2 values) would be three times what is calculated in the cumulative calculation. In this second example what is essentially happening is that we are allowing three times the PDE in each daily dose of the next drug product.
Now it may be that the actual measured residue in Example 2 would be acceptable because of the robustness of the cleaning process. Perhaps our measured residue values (corrected for sampling recovery values) were less than 33% of the calculated limit, which would result in the actual combined L2 (the sum from A plus B plus C) being acceptable. However, this is probably not a preferred approach. Among other things, it may require different sampling recovery studies to be performed to account for the different L3 limits.
However, it may be possible to set different L3 limits for different equipment items provided that a total L2 is first calculated which is then apportioned among the different equipment items. So this “stratified sampling” approach is different from Case 2. Case 2 involves setting separate L3 limits for each equipment item, while Case 3 involves different L2 values for each equipment item and then summing those individual values to arrive at a total L2 amount. The sum total of those L2 values is then compared to the calculated L2 value. The relative apportionment does not have to be based on surface area, but could be made on difficulty of cleaning or another factor such as historical residue data. Again, this type of apportionment could be made, but presents more complexity in implementation. So, while it is theoretically possible to use, I generally don’t recommend this approach.
If clarification is needed, please see the September 2012 Memo for a discussion of the shorthand “L series” to denote different ways to express limits.
© 2026, Cleaning Validation Technologies


